

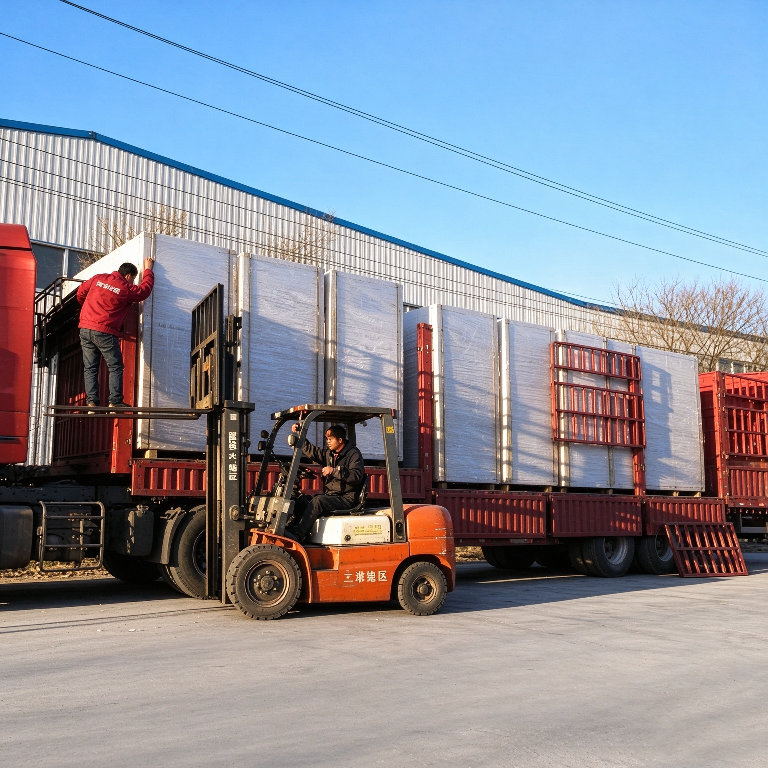
How Can Honeycomb Composite Panel Procurement Lock in Stable Lead Times Amid Plastic Raw Material Volatility?
The impact of plastic raw material volatility on honeycomb composite panel procurement rarely appears in the form of “panels being unavailable.” It more commonly follows this path: sharp rises or falls in PP resin prices → suppliers reorder production priorities and their raw material stocking rhythm is disrupted → quoted lead times quietly stretch from 15–25 days, or orders are accepted but goods are unavailable. By the time the buyer notices, the cost of a production line waiting for material has already occurred. Locking in lead times is essentially not about chasing suppliers for delivery. It is about arranging the supply structure, contract mechanisms, and buffer capacity before price volatility is transmitted to the delivery side.
The root of the problem is that honeycomb panel lead times are highly sensitive to changes on the raw material side. Polypropylene resin typically accounts for 35%–45% of the manufacturing cost of PP honeycomb panels, and in some hollow-profile board products the raw material cost share is close to 70%. This means that every significant fluctuation in resin prices will simultaneously affect suppliers’ raw material purchasing decisions and production scheduling. More critically, cost transmission lags significantly: raw material price increases occur first, while price adjustments at the panel stage often lag by weeks or even longer. During this time lag, if a supplier believes that raw material prices may rise further, it may tend to control the pace of order acceptance or prioritize orders with higher bids. If prices fall sharply, it may delay raw material purchases to wait for lower costs, which likewise disrupts the production sequence of existing orders. The root cause of unstable lead times is the disturbance of price signals. Simply applying pressure at the delivery stage has limited effect.
Layer 1: Choose the right supply structure and include “raw material stability” in supplier evaluation.
A honeycomb panel supplier’s ability to absorb raw material volatility first depends on its position in the industry chain. Manufacturers with vertical integration capabilities—from PP pellet extrusion of honeycomb cores and production of facing skins to lamination of finished products, all completed within their own factories—have stronger control over raw material stocking and production scheduling. By contrast, pure panel assemblers need to purchase honeycomb cores externally, while traders control neither the core material nor the lamination stage. Once upstream core supply tightens, their lead-time flexibility is the first to be compressed. In an environment of heightened raw material volatility, buyers should treat “whether the supplier produces honeycomb cores in-house,” “the level of常规 resin raw material inventory,” and “the on-time delivery record during periods of sharp PP price volatility over the past 12 months” as hard criteria for supplier admission, rather than comparing only per-square-meter quotations. The stability of lead times is already largely determined by the supplier’s industrial structure before production begins.
Layer 2: Use contracts to separate price risk from delivery obligations, and avoid “locking prices” turning into “failing to lock lead times.”
Under raw material volatility, the buyer’s most direct impulse is to sign a fixed-price contract and lock in the unit price for the next 6–12 months. But fixed-price contracts are precisely a high-risk area for delivery breaches when raw material prices surge: when suppliers face a cost inversion on raw materials, they either lack the incentive to perform at a loss or use “tight production scheduling” as an excuse to delay delivery. The buyer holds a fixed-price contract but cannot get the goods. A more pragmatic approach is to design the price mechanism and lead-time assurance separately. On the price side, an index-linked contract can be adopted, dynamically linking the panel unit price to an authoritative PP spot index or futures contract settlement price, so that both parties share the volatility. Suppliers no longer bear the raw material exposure alone, which reduces their incentive to sacrifice lead times because of cost inversion. In parallel, a lead-time assurance clause should be written separately into the contract: specify a capacity reservation ratio (for example, a certain proportion of the annual forecast volume as “reserved capacity”), agree on tiered liquidated damages for late delivery (distinguishing between delays within 5 days and those exceeding 5 days), and impose constraints that prevent suppliers from unilaterally changing the confirmed production sequence when raw material prices fluctuate beyond a certain range. Price is price; delivery is delivery. Governing them separately is actually more reliable than forcibly bundling them together.
Layer 3: Use dual buffers in inventory and capacity to absorb volatility, rather than using expediting to digest volatility.
Honeycomb panels’ normal lead times themselves have room for flexibility: standard products fall within a 15–25 day range, while custom specifications and peak ordering periods extend them further. At a stage when raw material price signals change frequently, waiting to place orders “only when needed” under a zero-inventory strategy is equivalent to pressing all volatility risk onto the delivery stage. Buyers need to establish layered buffers based on their own usage structure. For standard specifications, maintain safety stock of one or two commonly used thicknesses and sizes to absorb lead-time jumps caused by sudden insert orders and short-term raw material disturbances. For non-standard or project-based demand, designs should be brought as close as possible to the supplier’s existing standardized modules at the design stage, because non-standard products cannot be quickly reallocated in emergencies, whereas standard-sized panels can be allocated across warehouses under a supplier’s multi-site footprint. On the capacity side, prioritize suppliers with multiple production bases or multiple production lines, and reserve production slots before peak season through advance payments or framework agreements—during demand peaks in the honeycomb panel industry, lead times extending from the usual 7–15 days to more than 20 days are not uncommon. Reserving production sequence in advance is far more effective than expediting with temporary price premiums.
Layer 4: For companies with the necessary conditions, use financial instruments to “move” raw material cost uncertainty out of lead-time decisions.
For buyers with large PP resin exposure, the value of futures and options tools lies not in speculation but in the fact that once raw material costs are locked, neither suppliers nor buyers need to adjust production scheduling behavior by “betting on direction.” A path that small and medium-sized enterprises can refer to is a combination of “spot purchasing + options hedging”: purchase part of immediate demand in the spot market when prices are low, while buying call options for the remaining volume to cap the maximum procurement cost, or using a combination of buying calls and selling puts to reduce premium expenses. Once the upper limit of raw material costs is locked by tools, suppliers no longer have an incentive to delay delivery on confirmed orders to wait for more favorable raw material prices, and the predictability of lead times improves accordingly. The price-fixing purchase and sale model uses futures prices as a benchmark and completes spot settlement through a margin mechanism, which can likewise separate “when to buy raw materials” from the lead-time variable. The threshold for using such tools is declining. The key is whether buyers regard them as infrastructure for lead-time management rather than as purely financial operations.
Raw material volatility will not disappear, and the lead times of honeycomb composite panels cannot be “locked down” once and for all by any single measure. The feasible path is layered defense: filter out links with insufficient raw material control in supplier selection, decouple price risk from delivery obligations in contracts, retain a margin for absorbing volatility in inventory and capacity, and use tools to move cost uncertainty out of lead-time decisions. When these four layers are stacked together, lead times are no longer the result of repeated negotiations during every raw material disturbance, but an output that can be managed.